Process Capability · Cold Heading Replaces Machining
Cold Heading Replaces Machining: Cost-Down Conversion
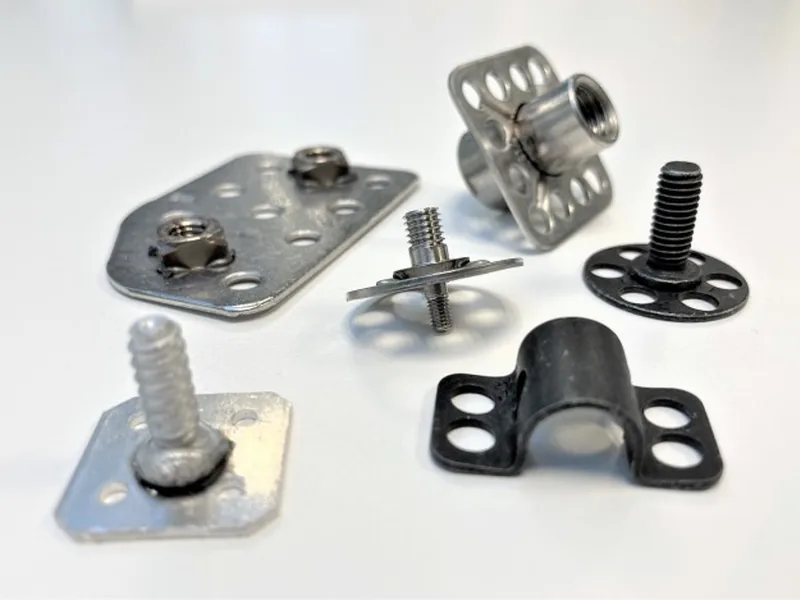
Converting machined parts to cold heading is the most direct cost-reduction path for fasteners and precision structural parts: continuous grain flow, work-hardening strength gains, high material utilization and fast takt; complex parts take the "cold-headed near-net shape + light machining" combined route.
5 Gatesexecutable process criteria
7%–10%strength gain vs machining, same steel
2 Routespure cold heading / combined
1 Dayfast sample arrangement
01
Why Convert Machining to Cold Heading
Machining is a subtractive process: whatever is turned away from the bar is discarded cost — a bin of chips is metal you bought and then cut off. The industry often cites the 15/85 total-cost rule of thumb: the direct purchase cost of the fastener is about 15% of the total joining cost, with the remaining 85% spread across design selection, assembly efficiency, quality rework and after-sales; and within that 15% of visible cost, material is usually the largest share — precisely the part cold heading can rewrite most. "Using CNC is safer for prototypes" holds true, but on a line producing hundreds of thousands of parts a year, it is often the most expensive option.
02
Cold Heading vs CNC: Five Dimensions
| Manufacturing factor | Cold heading (forming) | CNC (cutting) |
|---|---|---|
| Material utilization | High; only setup scrap | Low; chips on every part |
| Grain flow | Continuous, following the contour without breaks | Cut by the tool, forming a mechanical discontinuity |
| Strength (same material) | Markedly better (work hardening + continuous flow) | Yield/tensile strength reduced |
| Takt | Orders of magnitude apart; seconds per part | Slow |
| Upfront cost | High tooling cost; changeover 6–12 hours | Minimal tooling cost; setup 2–4 hours |
| Total cost at volume | Lower as volume grows | Suited to first articles and small batches |
| Geometric freedom | Limited by the forming envelope | Highest freedom |
03
Grain Flow: Cold-Headed Parts Are Naturally Stronger
Cold heading makes metal flow inside the die: grain flow wraps around the head, passes through the neck and runs through the shank, continuous and unbroken; turning cuts the flow at head-to-shank transitions and fillet steps, creating stress-concentration starting points. Measured comparison of turned vs cold-headed bolts of the same steel grade and size:
| Bolt size | Steel grade | Turned tensile (kgf/mm²) | Cold-headed tensile (kgf/mm²) | Improvement |
|---|---|---|---|---|
| M8 | Steel 40 | 62 | 68 | approx. +9.7% |
| M10 | Steel 35 | 56 | 60 | approx. +7.1% |
| M12 | Steel 40X | 60 | 65 | approx. +8.3% |
| M18 | Steel 35 | 52 | 57 | approx. +9.6% |
After heat treatment, the breaking load along the shank of cold-headed blanks is 10%–20% higher than for turned parts; more importantly, fatigue strength — cold heading reduces machining marks and keeps the grain flow continuous through corners, with fatigue strength gains especially pronounced at critical load-bearing corners.
Need "cold heading conversion" selection review or a quote?Specification sheet and selection advice provided, with one-to-one replies from engineers
04
Work Hardening: Dividend and Red Line
Cold heading plastically deforms metal beyond its yield point at room temperature — itself a cold-work hardening pass: the yield point, elastic limit and ultimate strength rise, some parts can meet spec with reduced or even no strengthening heat treatment, and surface hardness and wear resistance improve in step. The red line is equally clear: the greater the deformation, the more ductility is consumed; beyond the material's allowable deformation degree, the part cracks. There are three engineering responses: multi-station staged deformation, intermediate annealing to restore ductility, and selecting annealed/normalized wire. General thresholds for cold-heading wire: tensile strength generally not above 70 kgf/mm², elongation not below 12%, reduction of area not below 50%.
05
The Material Ledger and Takt
The bar diameter for turning must be no smaller than the part's largest diameter; a cold-headed part "grows" from wire at an intermediate cross-section close to the finished shape. A classic comparison for multi-station cold-heading equipment: for the same part, turning needs 3000 lbs of raw material per 1000 pieces, while cold-heading blanking needs only 326 lbs — on expensive materials such as SUS630, this material ledger often decides whether the project proceeds at all. On takt, cold heading and cutting differ by orders of magnitude; changeover takes 6–12 hours for cold heading versus 2–4 hours for CNC, so CNC for small-batch prototyping and cold heading for volume orders is the industry-standard combination.
06
Five Process Gates: Calculate Before You Convert
| Gate | Question to answer | Criterion |
|---|---|---|
| Gate 1 | Can the material take the deformation? | Is the deformation degree q below the material's allowable value (low-carbon steel 60%–70%, high-carbon steel only 20%–30%) |
| Gate 2 | How many blows are needed? | Free upset ratio S=L/D: ≤2.5 one blow, ≤4.5 two blows, ≤6.5 three blows |
| Gate 3 | Will the shank buckle? | Length-to-diameter ratio and ejection method: solid-die shank length not over 8d; beyond that switch to an open die or secondary machining |
| Gate 4 | Is the machine capable enough? | Three parameters: wire diameter, blank length and forming force (not "how big the head is") |
| Gate 5 | Does the wire meet spec? | Incoming inspection on four items: Brinell hardness, tensile strength, elongation, reduction of area |
If any of the first four gates is clearly exceeded, go straight to machining or a combined process; the fifth gate is the classic source of "it can be made but not stably" — the root of yield problems is often the incoming wire.
07
Two Core Calculations: Deformation Degree and Blow Count
Deformation degree q measures how much one forming pass changes the material: q = 1 − (d/D)² (d is the original wire diameter, D the upset diameter). For example, φ5mm wire upset into a φ10mm head gives q = 1 − (5/10)² = 75% — only low-carbon-steel-grade materials can take that deformation; the higher the carbon and alloy content, the lower the allowable deformation degree.
| Extrusion method | Max area reduction per pass | Max extrusion angle | Typical use |
|---|---|---|---|
| Open extrusion (blank pushed through into a smaller hole) | ≤30% | ≤30° | Bolts, screws, stepped shafts |
| Closed (confined) extrusion | Up to 75% | — | Larger head-to-shank diameter ratios: nuts, sleeves, hollow rivets |
Follow the table above when the shank must be extruded down; the "extrude the shank first, upset the head second" combination lets the head-to-shank diameter ratio exceed the single-blow upset limit of 2~2.5. If S=L/D is too large and a single upset is forced, the section of blank sticking out of the die buckles first and then folds over, forming a cold shut (lap) — on the surface it is a crease, but internally the material is actually discontinuous; it is the most dangerous cold-heading defect and becomes a crack source under heat treatment or load.
08
Combined Route: Machining Conversion + Light Cold Heading
When part geometry exceeds the cold-heading envelope or key geometric tolerances are extremely tight, there is no need to choose one or the other — "cold-headed near-net shape + light machining" is the best-value combined route:
- Forming goes to cold heading: keep the grain-flow and work-hardening dividends, turning over 90% of the material into the part instead of chips;
- Precision goes to machining: only key fitting dimensions and geometric tolerances receive precision turning/grinding, with allowances greatly reduced;
- Typical chain (SUS630 / 17-4PH): solution-annealed wire → multi-station cold-headed near-net shape → thread rolling → aging → light finish machining. Aging comes with about 0.04%–0.06% dimensional shrinkage; any machining with geometric or dimensional requirements must be scheduled after aging;
- Economics: machining hours drop from the whole part to a few features, while material utilization and takt still count as cold heading — the larger the volume, the clearer the combined route's advantage.
Need "cold heading conversion" prototyping or volume supply?Drawing review, rapid prototyping and volume scheduling handled end to end
09
Case Studies
Two completed machining-conversion cases
- 6061 battery pack lifting sleeve: pure CNC machining from bar stock would cut the aluminum's grain flow, leaving weak points under cyclic stress; after conversion to cold heading, the grain flow wraps continuously around the flange and body, and tensile testing showed higher resistance to stress fracture — for a lifting point carrying the weight of the whole battery pack, that is safety margin;
- VA/VE process cost-down: internal accounting of a forging-to-cold-heading project showed a unit cost reduction of CNY 0.75, totaling CNY 375,000 across 500,000 parts.
10
Industry Applications
Cold-heading-to-machining conversion capability serves new-energy vehicles (battery pack structural parts, lifting points), enclosures and cabinets (turned parts, welded-nut-type special parts), and precision structural parts for industrial and consumer electronics; mature cold-heading process reserves exist for stainless steel (SUS630/316L/302HQ), carbon steel, alloy steel and aluminum alloy wire.
11
Summary and Service
Leave "can it be cold headed" to the five gates and "is it worth converting" to the volume and total-cost ledger. Send us the drawing; we will calculate gate by gate and give a pure cold heading / cold heading + light machining route recommendation with a quote; small-batch fast samples can be arranged in as fast as 1 day.
Company Information
Yingfeng Zhichengjia Precision Hardware (Shenzhen) Co., Ltd. | HQ: Room 101, Building C1 and the whole building, No. 13 Kengzi Zhongxing Road, Xiuxin Community, Kengzi Street, Pingshan District, Shenzhen. Tel: 0755-84061349
Zhichengjia Metal Technology (Xiangyang) Co., Ltd. | Automotive-dedicated plant: Sanchalu Economic Development Zone, Chengguan Town, Gucheng County, Xiangyang City, Hubei Province. Tel: 0710-7269998
Website: www.zcjtech.com
Need a cold-heading cost-down assessment?
Provide the part drawing and annual demand; a process route recommendation and cost-down estimate within 1 working day; small-batch samples arranged in as fast as 1 day.