Tangless Inserts Product Manual
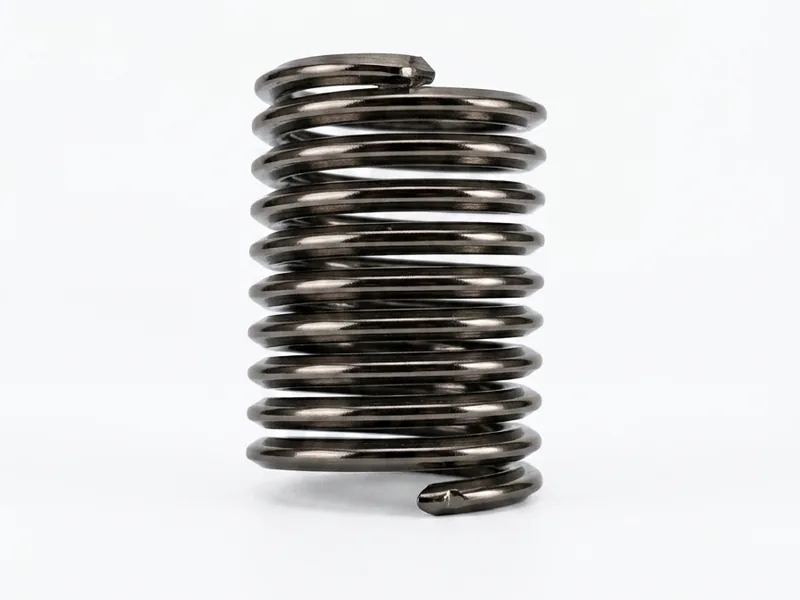
Tangless inserts (tangless wire thread inserts) have no installing tang: after installation there is no tang-breaking step and no debris left behind, ideal for blind holes, cleanroom and automated assembly; the full M2–M39 range with SUS304/SUS316/phosphor bronze/INCONEL options.
Product Overview
Thread Reinforcement Principle and Performance Data
- Higher internal thread strength in light alloys: effectively raises the internal thread strength of light alloys such as magnesium and aluminum to grade 12, allowing light-alloy tapped holes to mate with high-strength bolts of grade 8.8 and above;
- Even load distribution: without an insert the first thread carries about 50% of the load; with an insert the internal thread carries load more evenly, eliminating stress concentration;
- Material strength: wire thread inserts are usually made of hardened stainless steel (e.g. SUS304, hardness HRC 43–50) with tensile strength generally not below 1370MPa — light yet strong;
- Vibration and wear resistance: the elastic thread profile absorbs vibration energy, and the wear-resistant thread significantly extends repeated assembly/disassembly life.
Comparison with Tanged Inserts
| Item | Tanged wire insert | Tangless insert |
|---|---|---|
| Installation steps | Tang must be broken off with a breaking tool after driving (an extra step) | Installation is complete once driven — no tang breaking |
| Tang debris | Tang breaking produces debris; cleaning and verification needed | No debris left behind; no cleaning required |
| Blind-hole suitability | The tang occupies the bottom space; blind holes often must leave room for it | Blind holes can be fully used up to the maximum engagement depth |
| Automated assembly | Requires an extra tang-breaking step | Fewer steps; suited to automated lines |
| Cleanliness-critical settings | Tang debris must be tightly controlled | Better suited to clean assembly in optics, hydraulics, etc. |
Installation Process
- 1. Drilling: drill the tap drill hole at the diameter required for wire thread inserts, avoiding reverse countersinking where possible;
- 2. Tapping: tap the base material with the dedicated wire thread insert tap;
- 3. Thread check: the base thread can be checked with a thread gauge;
- 4. Installation: drive the tangless insert into the base thread with the installation tool, with the end about 1/4 turn below the surface;
- 5. Check: after installation, re-check thread go/no-go.
Tap Drill Design Points
- Drilling depth: the minimum drilling depth "S" must leave one thread pitch of chip clearance between the tap tip and the bottom of the hole; increase the drilling depth further when using spiral-point taps;
- Countersink: provide a 120° countersink before tapping to prevent the insert's leading threads from contacting sharp burrs;
- If countersinking is not possible: remove any burrs or deformed material at the leading threads before tapping, to ensure smooth installation and reduce operational impact;
- Drill selection: standard-size drills are recommended; drill sizes are recommended values — confirm by trial machining in the actual base material.
Product Features
| Feature | Description |
|---|---|
| Material | Stainless steel SUS304 / SUS316, phosphor bronze, high-temperature INCONEL nickel-base alloy |
| Size range | M2–M39, coarse and fine pitch |
| Length | Five standard lengths 1D / 1.5D / 2D / 2.5D / 3D, customizable |
| Types | Standard and locking versions |
| Surface finish | Lubrication, tin plating, zinc plating, silver plating (for high temperature), etc. |
| Color coding | Can be color-marked red, green, etc. on request, for easy spec identification on the line |
Locking and Color Coding
Typical Applications
- Blind holes: the tang no longer occupies the hole-bottom space, so thread utilization is higher;
- Cleanliness and hermeticity: assemblies in optical instruments, hydraulic components, medical devices, etc. where no metal debris can be tolerated;
- Automated lines: no tang-breaking step or debris cleaning, faster takt;
- Light-alloy repair and reinforcement: stripped-thread repair and thread reinforcement in aluminum and magnesium housings.
FAQ
Q1Tangless or tanged — how to choose?
Choose tangless first for blind holes, high cleanliness requirements and automated lines; for through-hole applications both work — trade off line process and tang-breaking cost.
Q2Does installation require tang breaking?
No. Tangless inserts have no installing tang; driving them in with the installation tool completes installation, with no debris left behind.
Q3How much thread strength gain?
The same as the wire thread insert system: internal thread strength in light alloys can be raised to about grade 12, mating with bolts of grade 8.8 and above; the tensile strength of hardened stainless steel wire is generally not below 1370MPa.
Q4What to watch for in the tap drill?
Drill to the tap drill size of the dedicated tap; the minimum drilling depth must leave one thread pitch of chip clearance for the tap tip; a 120° countersink before tapping is recommended, and where countersinking is impossible, burrs at the leading threads should be removed.
Q5What are the lead times?
Standard specs and lengths are scheduled by order; small-batch fast samples can be arranged in as fast as 1 day; special materials (e.g. INCONEL) and custom lengths are subject to process evaluation.
Industry Applications
Summary
Need tangless insert selection support?
Provide thread spec, length and base material; selection advice and a quote within 1 working day; small-batch samples arranged in as fast as 1 day.